




Sheet-Metal Part Detailing and Flat Patterns Folded shape, flat pattern.
A sheet-metal part exists in two states: the folded shape it becomes and the flat shape it starts as. The relationship between them is not obvious, it is specific to the brake and the tooling that will form it, and getting it wrong wastes material one part at a time until somebody checks.
What the deliverable contains
- Formed part drawings
- With dimensions in the folded state, which is how the part will be inspected.
- Flat pattern development
- With bend lines and bend direction identified, not merely implied by geometry.
- Bend allowances and deductions
- Applied to the parameters your fabricator supplies.
- Material specification.
- Type, gauge and finish, with the visible faces identified.
- Hole and cut-out positions
- Dimensioned in the flat state where fabrication needs them there, and in the folded state where inspection needs them there.
- Bend sequence
- Wherever the order is constrained by tooling access.
- Weld and fastening preparation
- Where applicable.
- Finish requirements
- Including which surfaces are exposed in the finished assembly.

Why bend parameters have to come from you
Bend allowance depends on the material, the gauge, the inside radius, the tooling and the machine. The same nominal part formed on two different brakes with different tooling produces two different flat patterns, and only one of them is correct for your shop.
So flat patterns are developed to the parameters your fabricator supplies: material and gauge, inside radius, and either the k-factor or the bend deduction table actually in use.
Where those are not available, that is said rather than a generic figure being applied quietly. A generic k-factor produces parts that are close, which is worse than parts that are obviously wrong, because close parts reach assembly before anyone notices.
A first article should always be checked before a production run, whoever produced the pattern.
Fixture sheet metal is not machine-guard sheet metal
The difference matters and it is where generic sheet-metal detailing falls down on fixture work.
- Visible surfaces.
- Bend marks, tooling witness and material grain direction all show on a display fixture under retail lighting. On a machine guard nobody looks.
- It has to receive something made from wood.
- Connection points are positioned and toleranced for the panel, shelf or upright they will carry, which is a different exercise from positioning them for another metal part.
- Finish adds thickness.
- Powder coating builds up on every surface including the ones that were dimensioned for clearance, and that clearance is usually where a wood component was meant to sit.
- Springback is real.
- Formed parts do not exactly match nominal geometry. On a fixture assembly, that variance lands at the interface, which is why adjustment provision belongs in the detail rather than in the fitter’s judgement.
Where it meets the wood scope
Flat pattern geometry exports as DXF for cutting. The formed parts sit inside the fixture assembly as one modelled set rather than as a separate metal package.
And the connection points those parts carry are detailed at the metal-to-wood interface, which is where a fixture usually fails if nobody owns it.
Who this is for
Fixture manufacturers with in-house or partnered metal fabrication. Millwork shops that added or bought a metal line and need drawings that match the new reality. Metal shops that took on wood and found the casework side harder than expected.
If your shop recently became a both-trades shop, this is the drawing problem you have been living between two vendors.
Selected work
Flat patterns developed to stated parameters
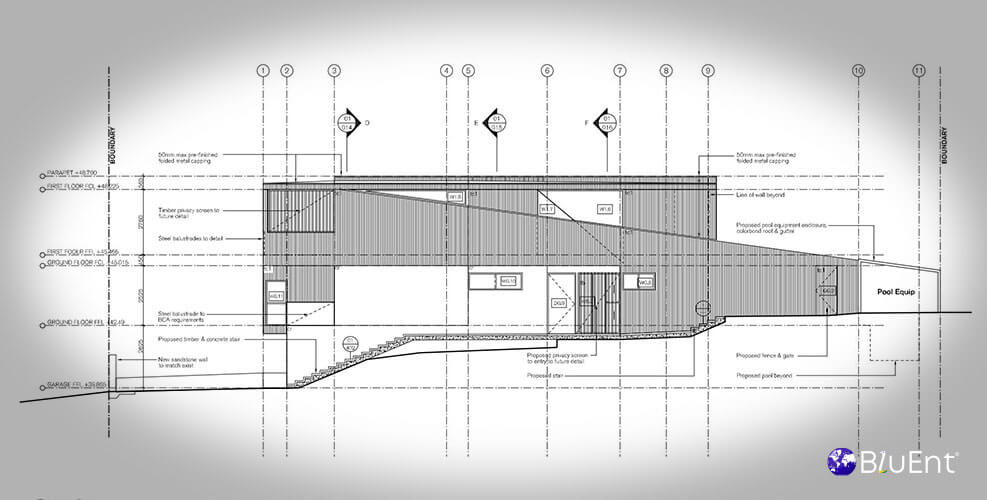
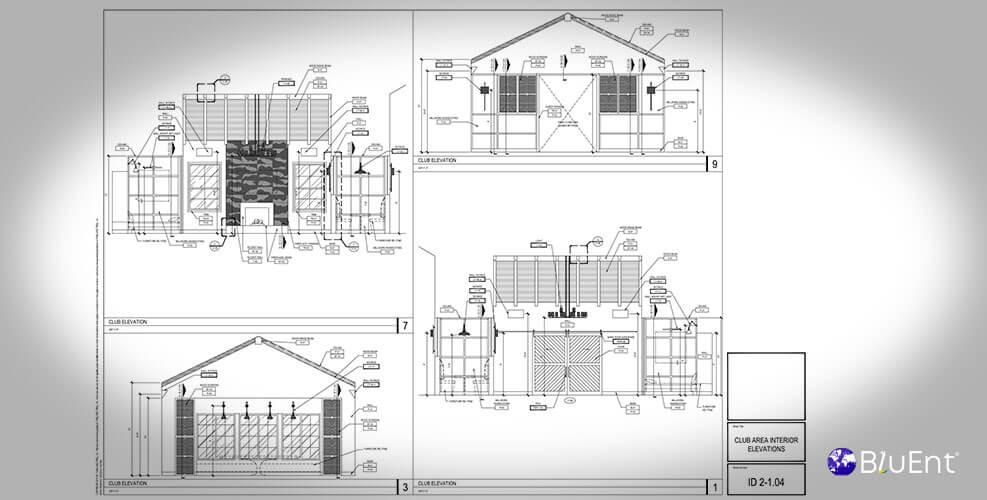
A generic k-factor produces parts that are close, which is worse than parts that are obviously wrong.
FAQ
Frequently Asked Questions
Do you supply flat patterns as DXF?
Yes, to your layer convention, alongside the formed part drawings. The two are produced from the same source so they cannot disagree.
What if our fabricator has not supplied bend parameters?
Then the assumption made is stated plainly on the drawing rather than buried. A first article should be checked before any production run.
Can you detail sheet metal outside a fixture context?
This service is scoped to fixture and millwork assemblies. General sheet-metal fabrication detailing is a different discipline with a different buyer and it is not offered.
Do you detail the welded frames as well?
Tube and brake-formed members are detailed for fabrication. Welded assemblies are detailed with our fabrication specialists where the scope requires it. See welded frame detailing.
Send one fixture component and your bend parameters
The detailed part and its flat pattern come back for your fabricator to check against their own brake.
- Formed part drawings and flat pattern from the same source
- Bend allowances applied to your fabricator’s stated parameters
- DXF supplied to your layer convention alongside the drawings
- One named contact, not a general queue
Project enquiry
Scope and questions come back, not a template.